Discover our elite tier of high-performance thermal imaging, PTZ surveillance arrays, and robust communication base stations engineered for extreme environmental durability.
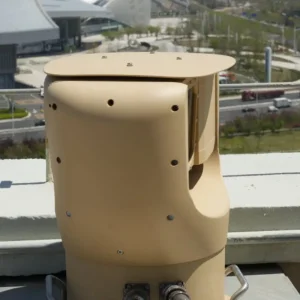
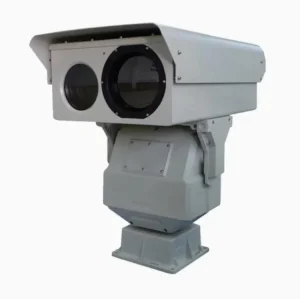

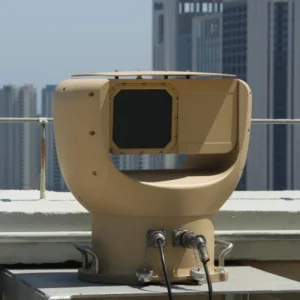
Comprehensive analysis of semantic parameters, search intent mining, and global manufacturing standards in modern intelligent security infrastructure.
Changzhou HawkEye Camera Co., Ltd. is a leading technology-driven enterprise specializing in the design, development, and production of advanced intelligent security and monitoring systems. With a robust foundation in innovation and cutting-edge technology, the company is committed to delivering high-performance, stable, and reliable products to meet the diverse needs of global markets.
Innovation and Expertise:
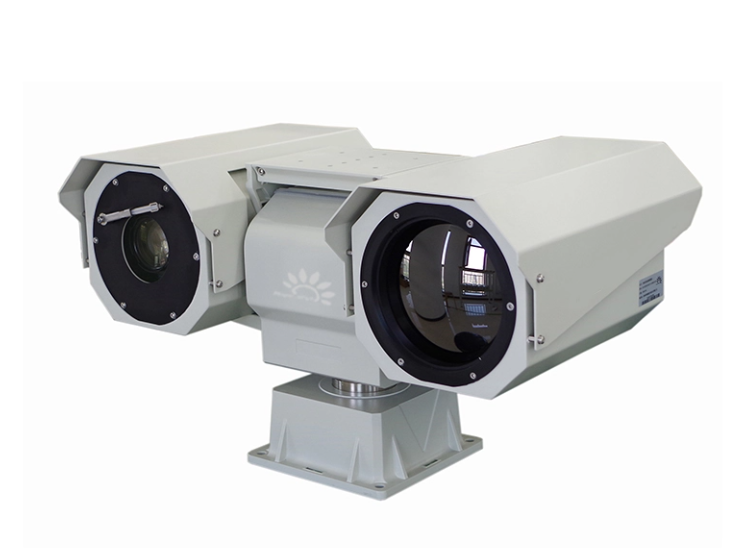
HawkEye Camera Co., Ltd. has established itself as a pioneer in the security industry, with a strong focus on research and development. The company boasts a highly skilled team with years of expertise in designing state-of-the-art security solutions. Our extensive product portfolio includes industry-leading products such as:
These products are widely used in critical industries such as transportation, public security, border defense, airport security, forest fire prevention, environmental protection, maritime safety, power management, urban management, and more.
Analyzing international purchasing demands, localized compliance, and technology roadmaps for next-gen integrated monitoring stations.
Modern international buyers demand turn-key integrated stations combining solar autonomy, multi-spectral thermal imaging, AI edge analytics, and ultra-reliable wireless transmission for remote deployments.
Adhering strictly to global quality frameworks, our systems hold ISO9001, CE, RoHS, and FCC certifications, ensuring hassle-free clearance and deployment across municipal, defense, and industrial sectors worldwide.
Integrating 5G IoT telemetry, deep-learning auto-tracking, and eco-friendly power subsystems under our flagship brand strategy: "HawkEye Security", leading the worldwide intelligent surveillance revolution.
Quality and Certification:
At HawkEye Camera Co., Ltd., we prioritize quality at every stage of production, ensuring that every product meets the highest international standards. The company’s manufacturing process adheres to strict quality control measures, ensuring product reliability and safety. All our products undergo rigorous testing at the Safety and Police Electronic Product Quality Inspection Center, and they meet the required national and industry standards.
The company is ISO9001 certified, and our products carry CE, RoHS, and FCC certifications, underscoring our commitment to quality, safety, and environmental responsibility.
Global Reach and Expansion:
Headquartered in Changzhou, Jiangsu, with branch offices in key cities like Shenzhen, Guangzhou, and Beijing, HawkEye Camera Co., Ltd. has developed a comprehensive marketing and service network. We are expanding rapidly into international markets, strengthening our presence globally while providing world-class products and services.
Commitment to Sustainable Development:
Guided by a philosophy of "Sustainable Development" and a "People-oriented" approach, HawkEye Camera Co., Ltd. strives to create a positive impact in both the industry and society. We are dedicated to maintaining a good corporate image and continuously improving our products and services through innovation. Our business philosophy emphasizes quality, reputation, and social responsibility, with a clear focus on promoting ethical management and environmentally-conscious practices.
Future Outlook:
With a forward-thinking vision, HawkEye Camera Co., Ltd. is ambitiously advancing its global brand strategy, "HawkEye Security", as part of its mission to become a world leader in intelligent security solutions. We will continue to invest in research and development, enhance our product offerings, and expand our global footprint, while remaining true to our core values of quality, customer satisfaction, and innovation.
Explore our complementary mobile surveillance units, ruggedized enclosures, mini-cameras, and specialized industrial components.

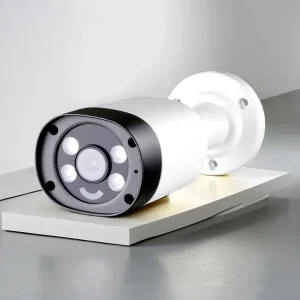
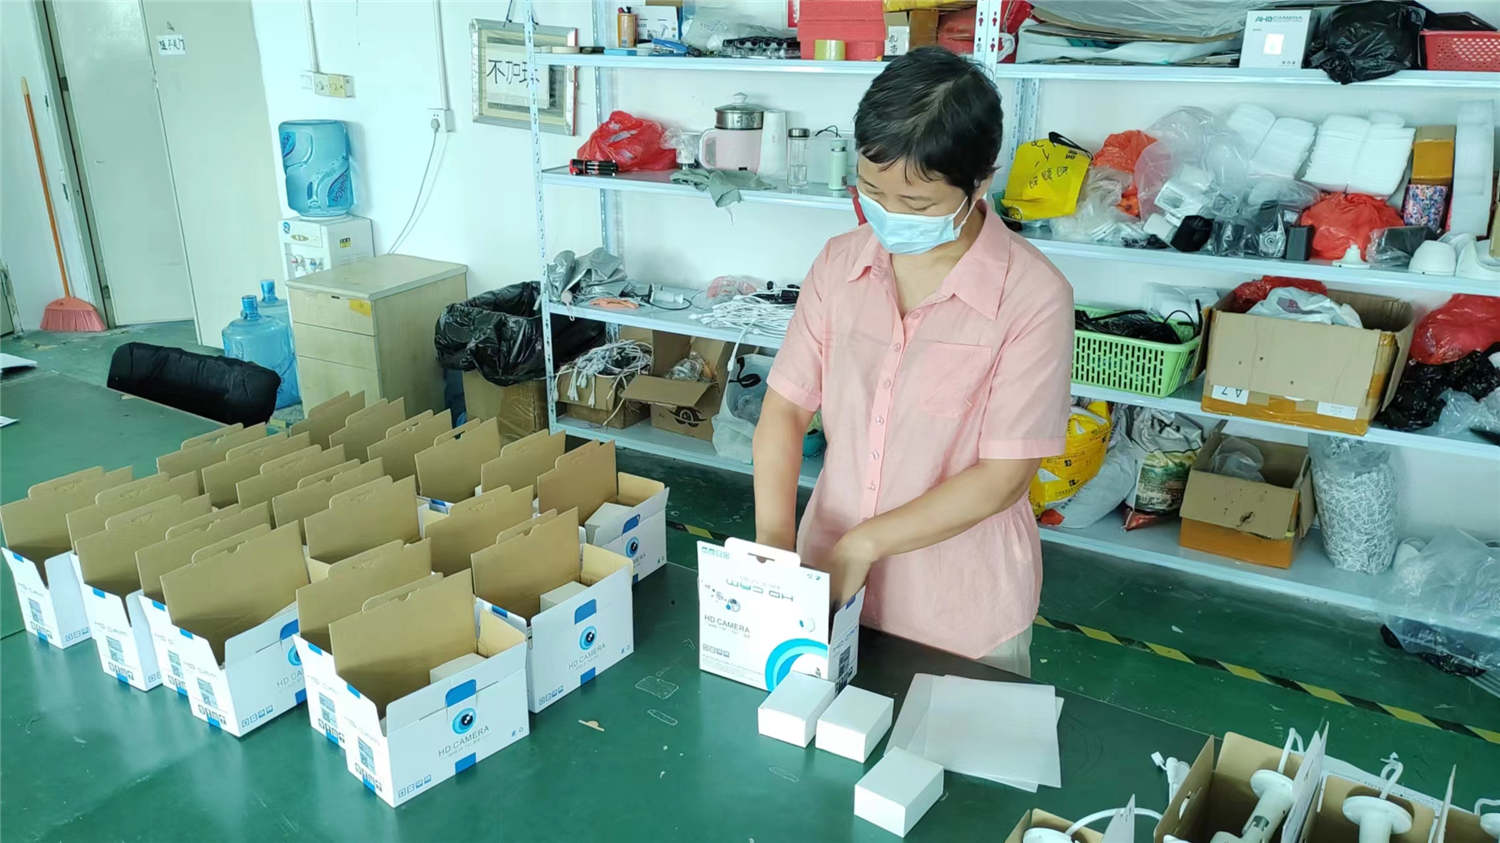
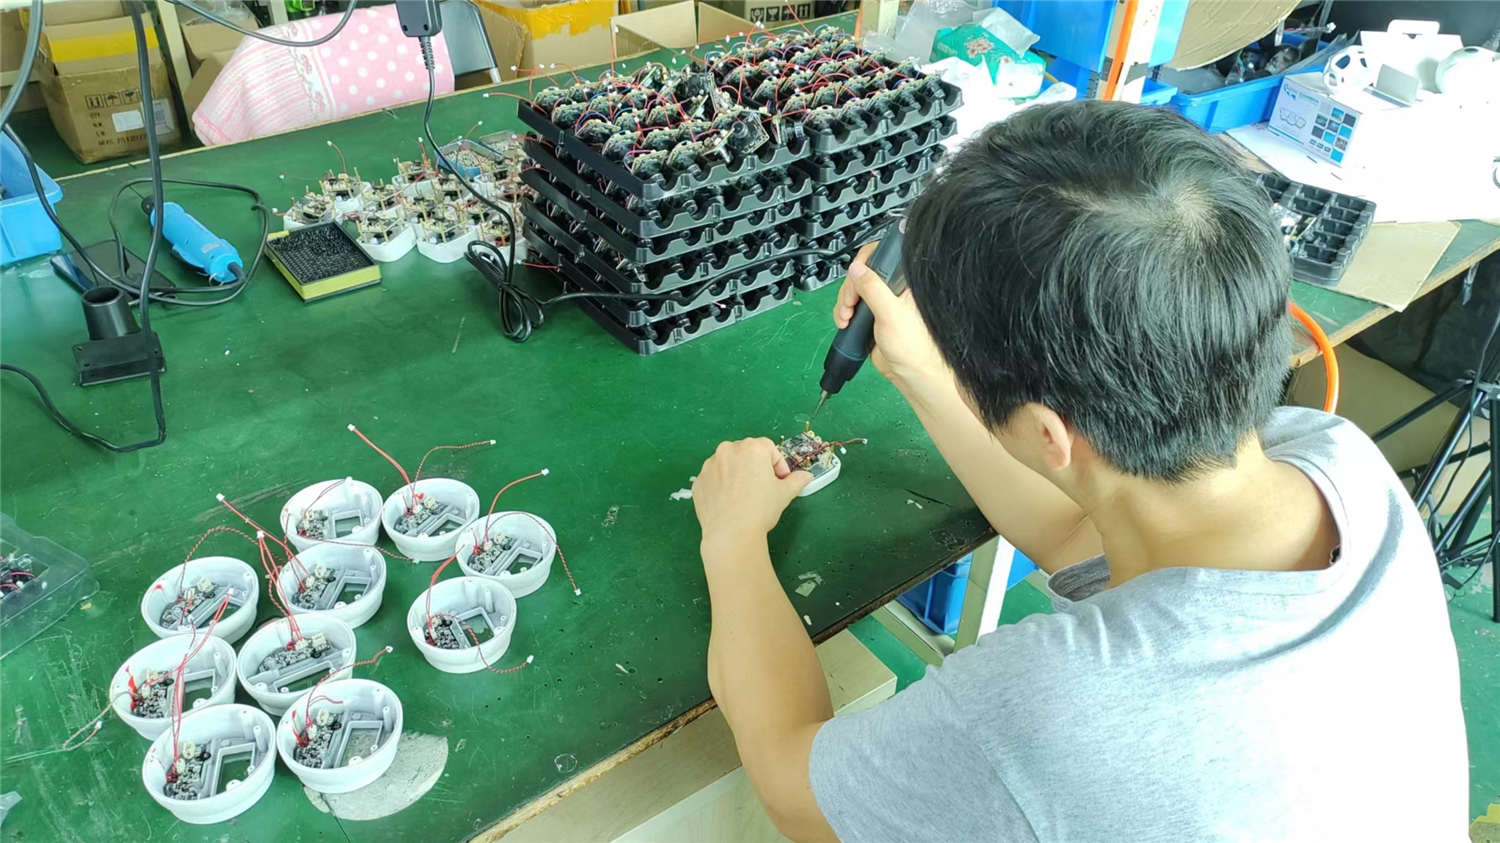
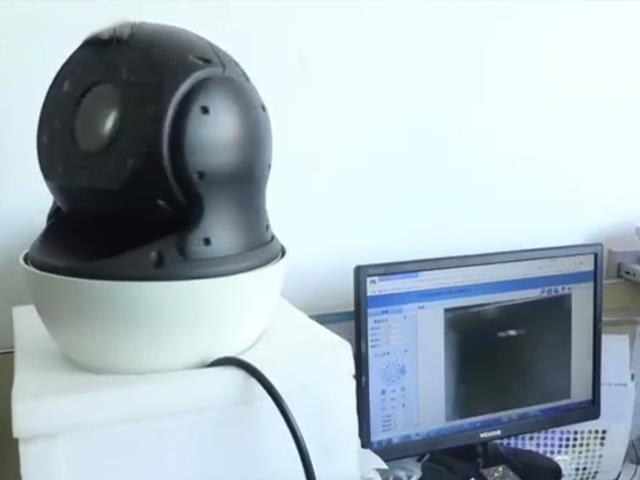
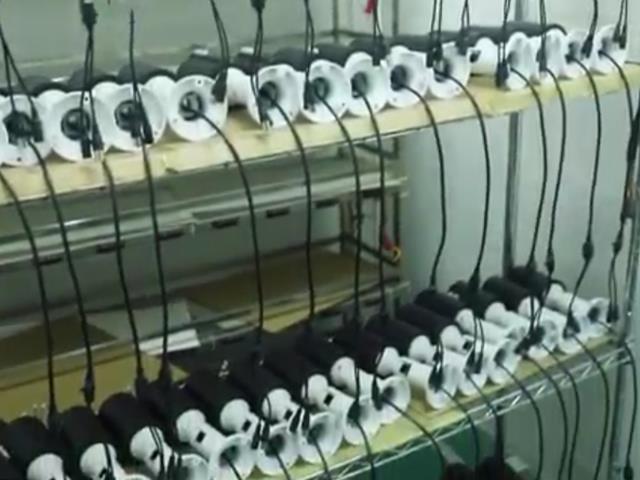
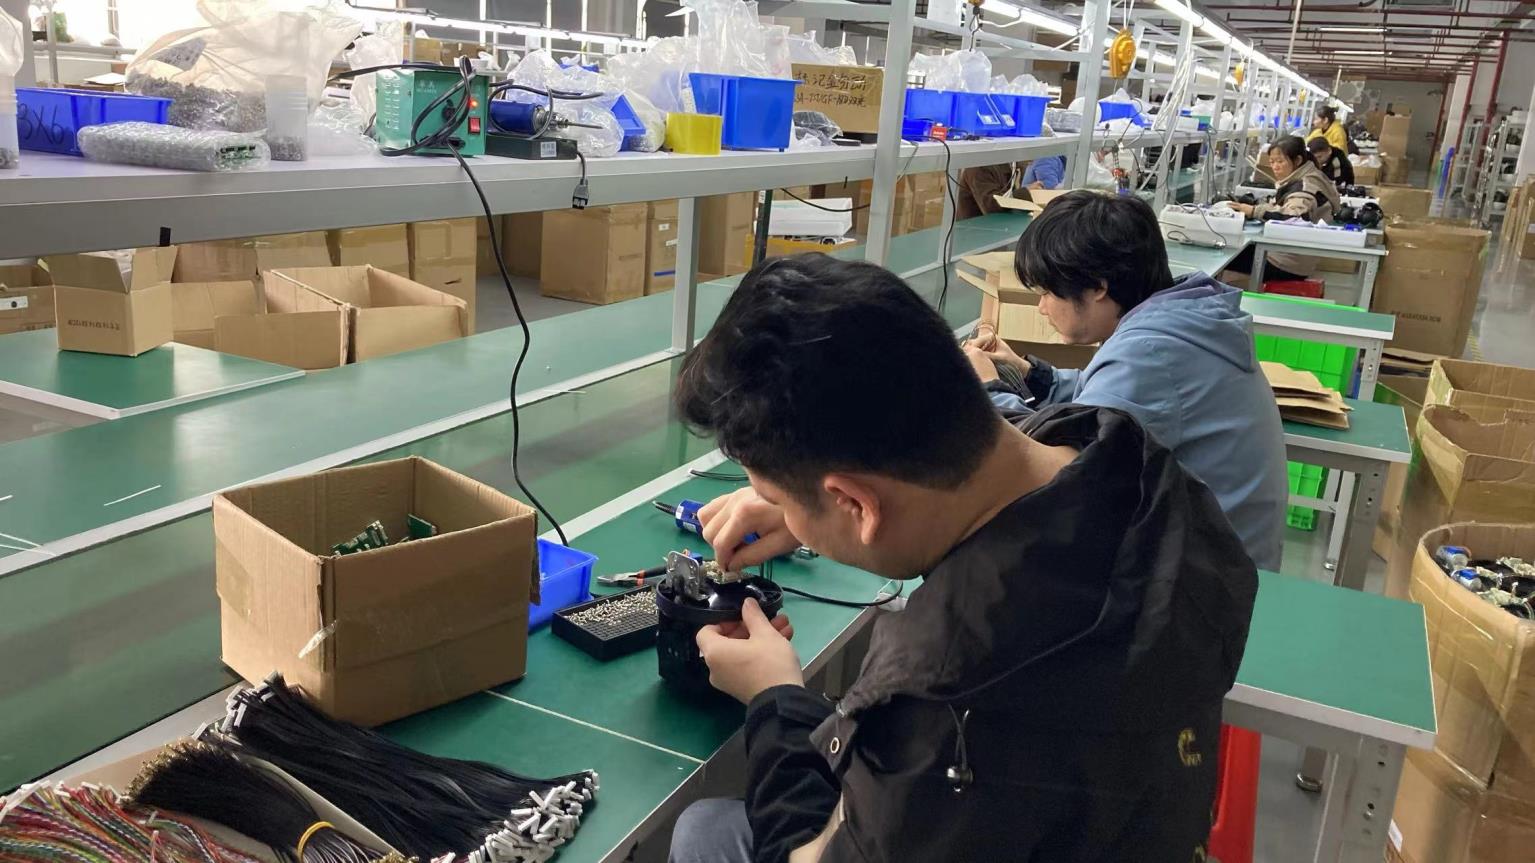
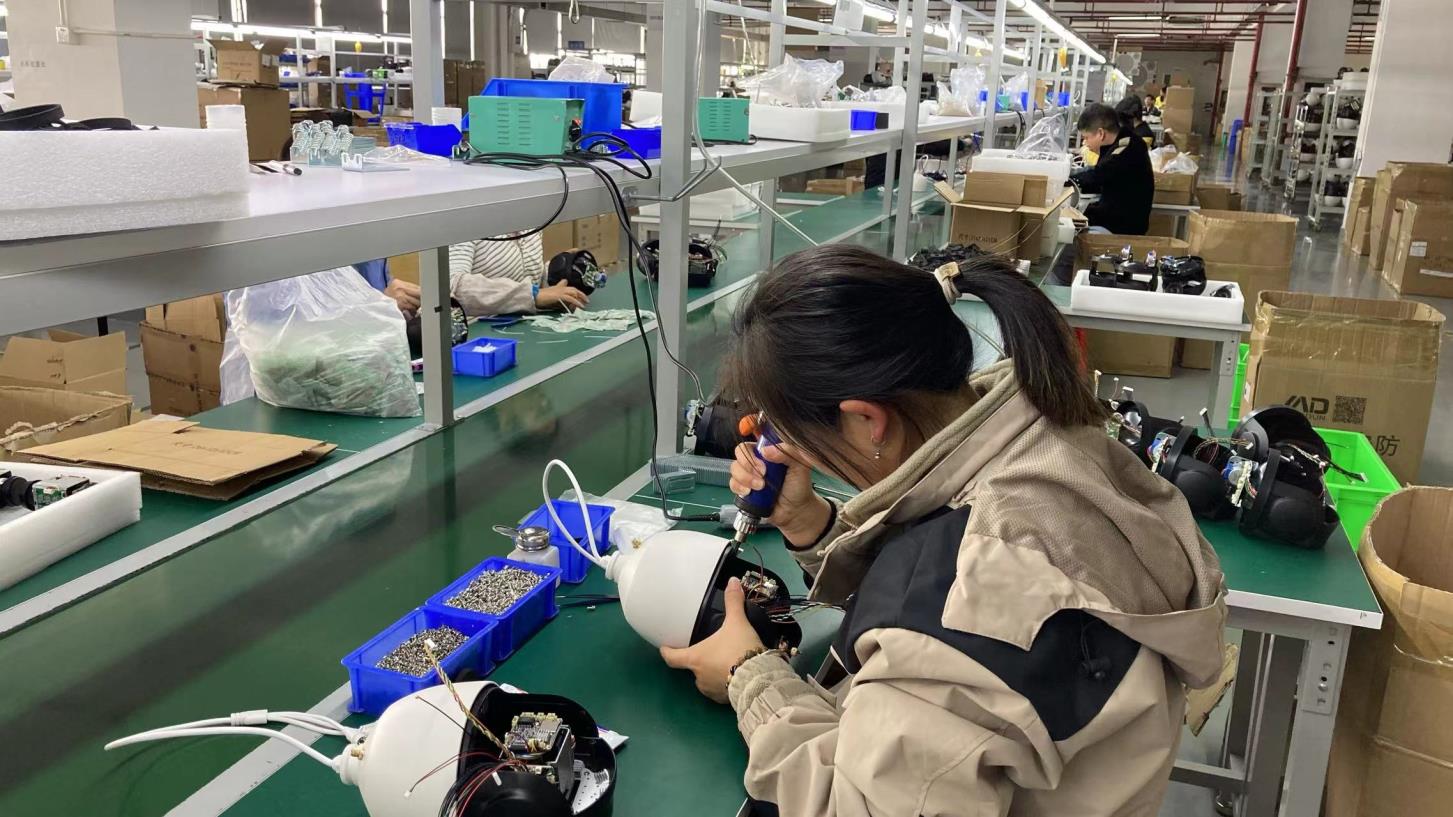
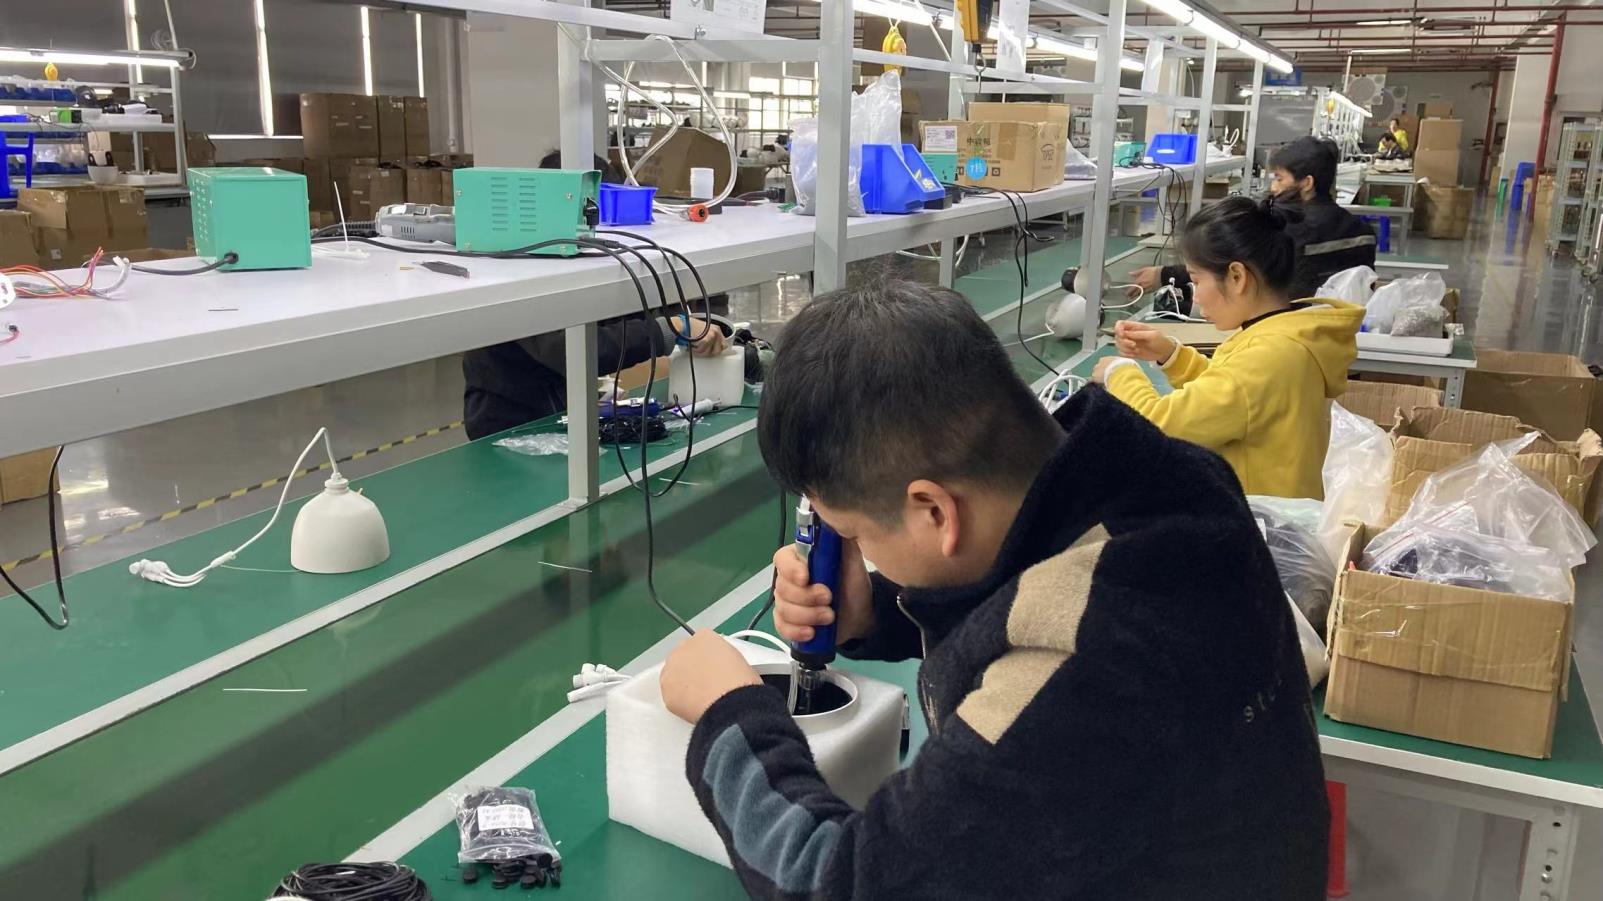
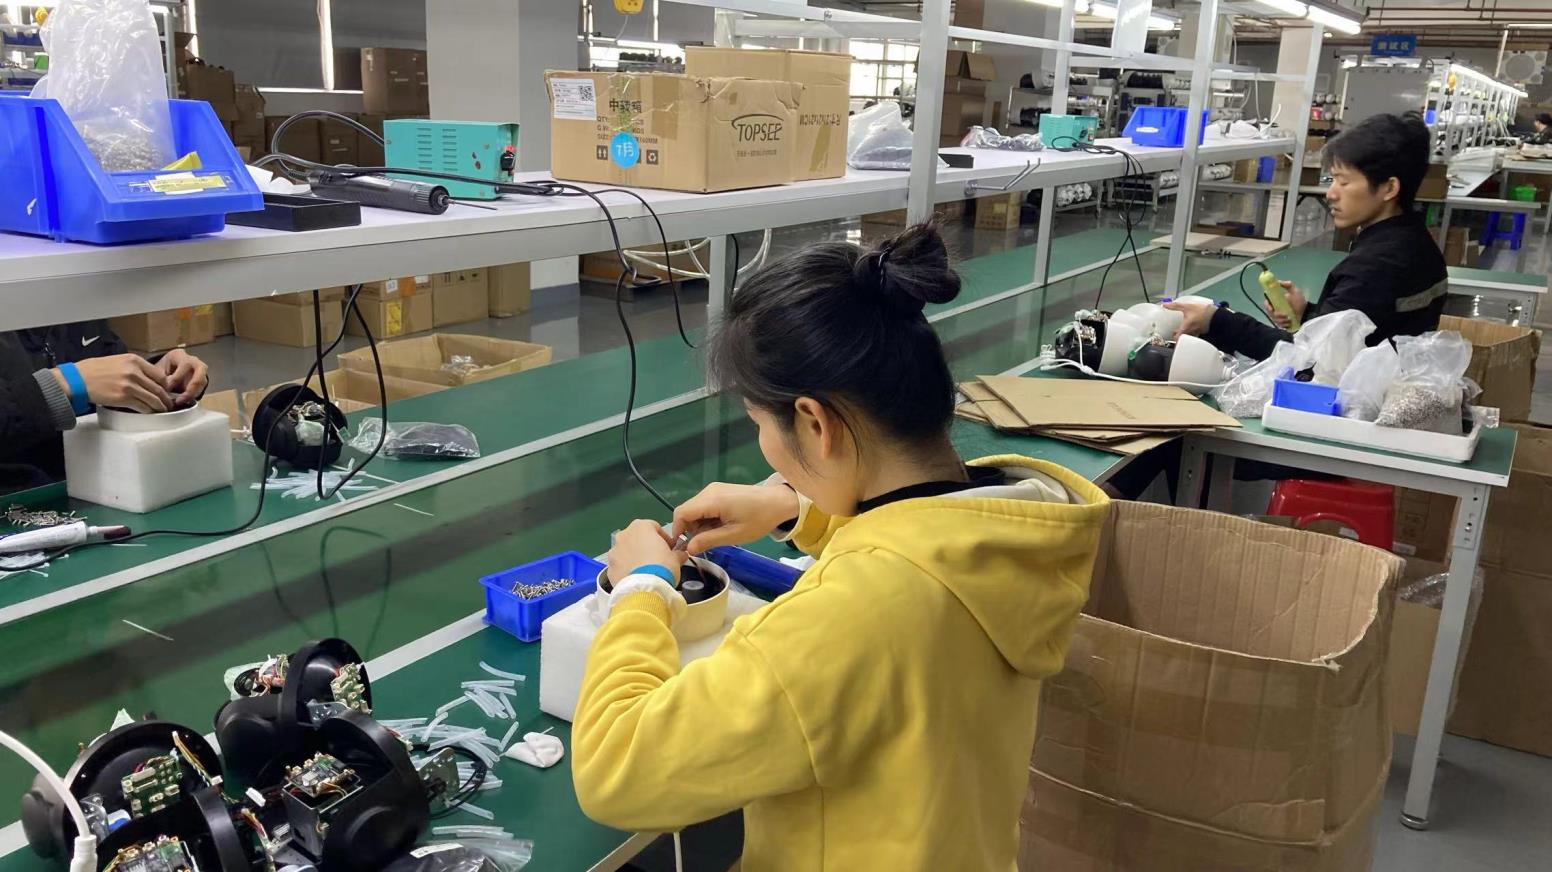
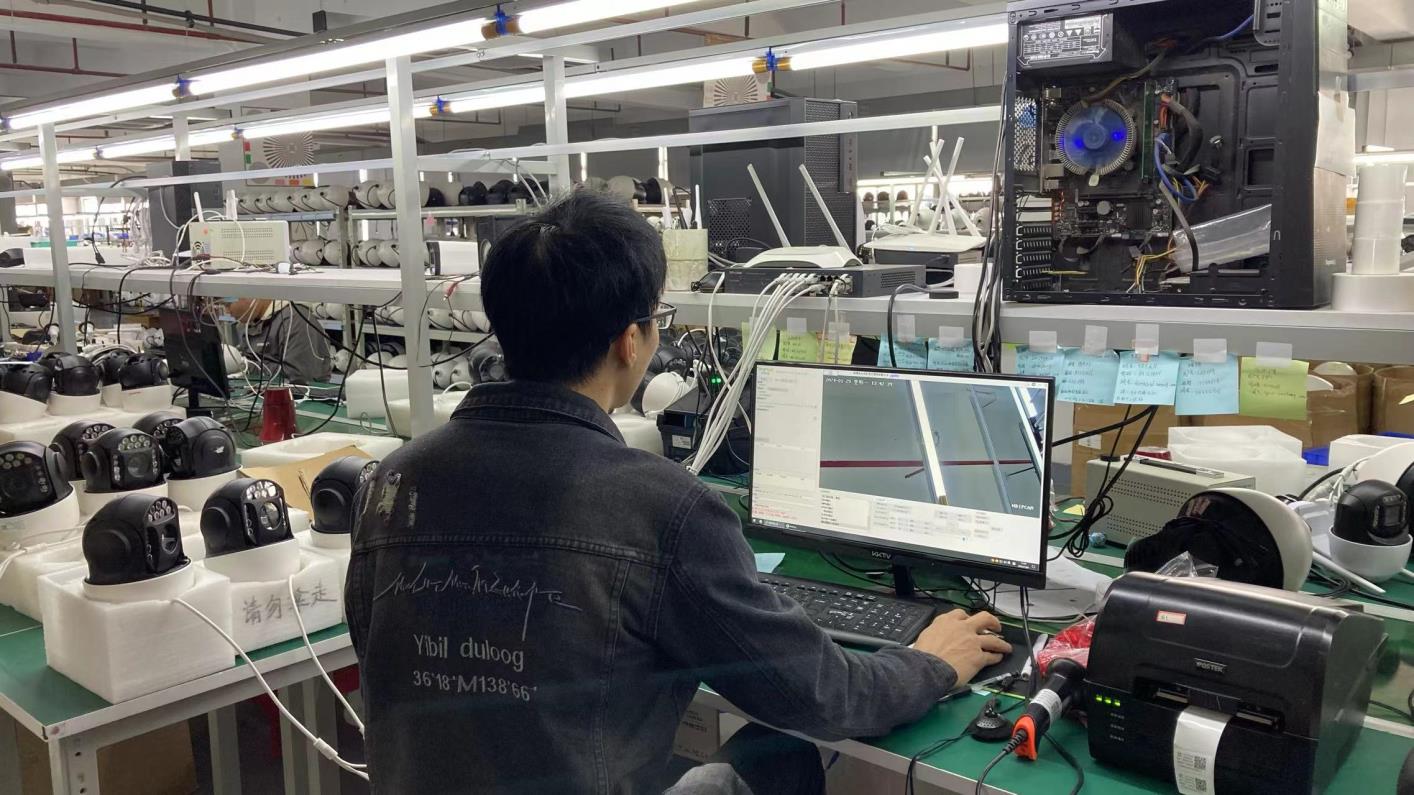
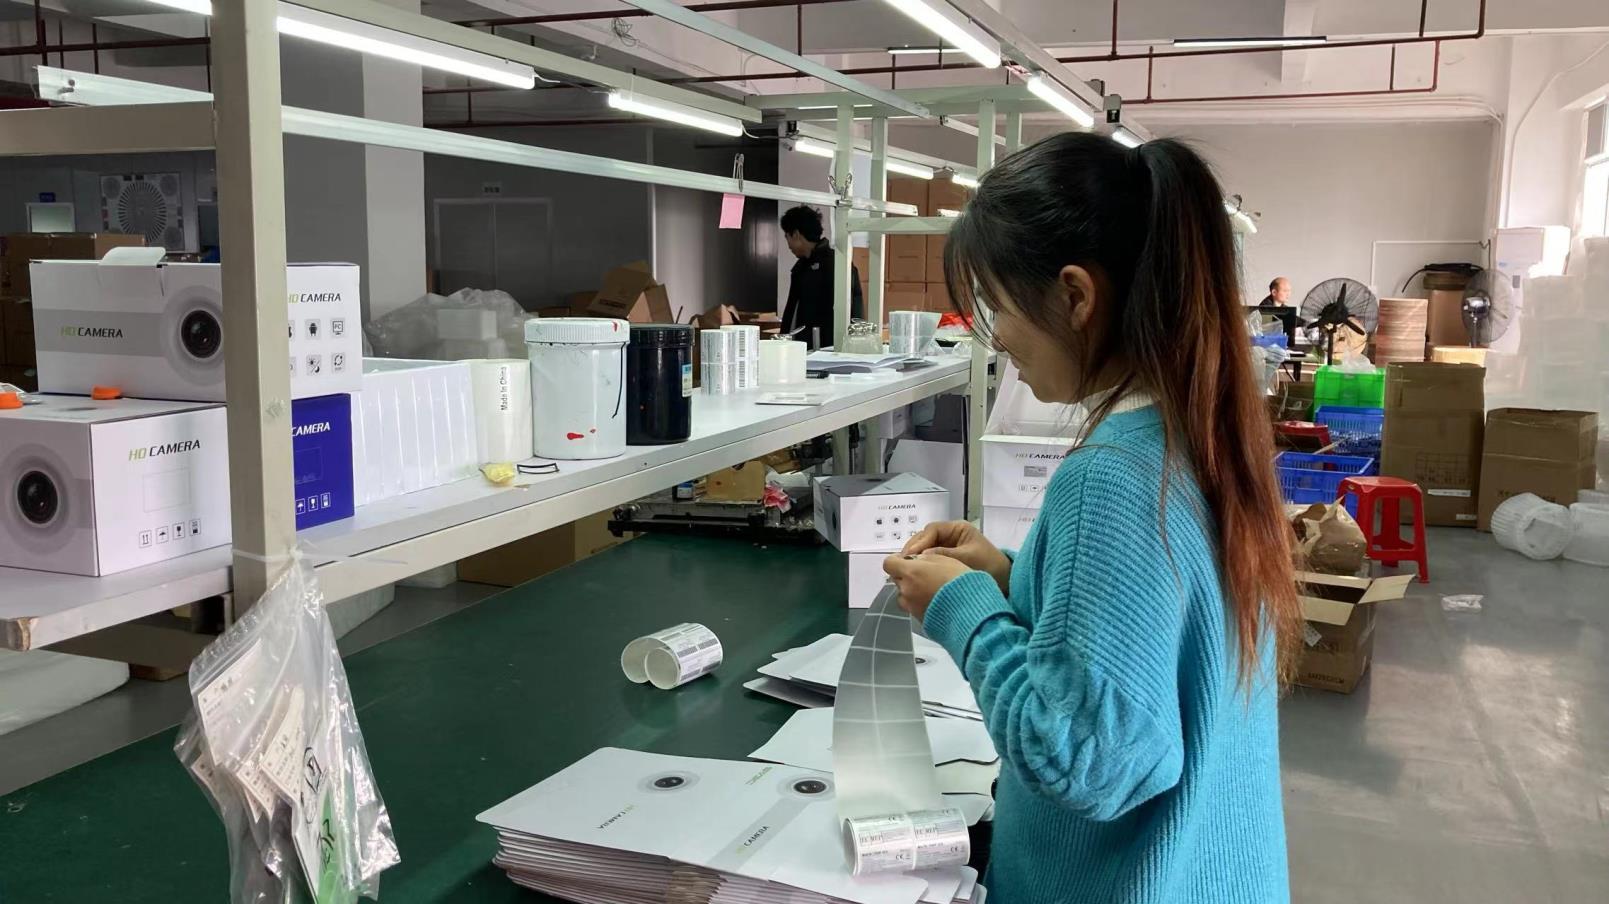
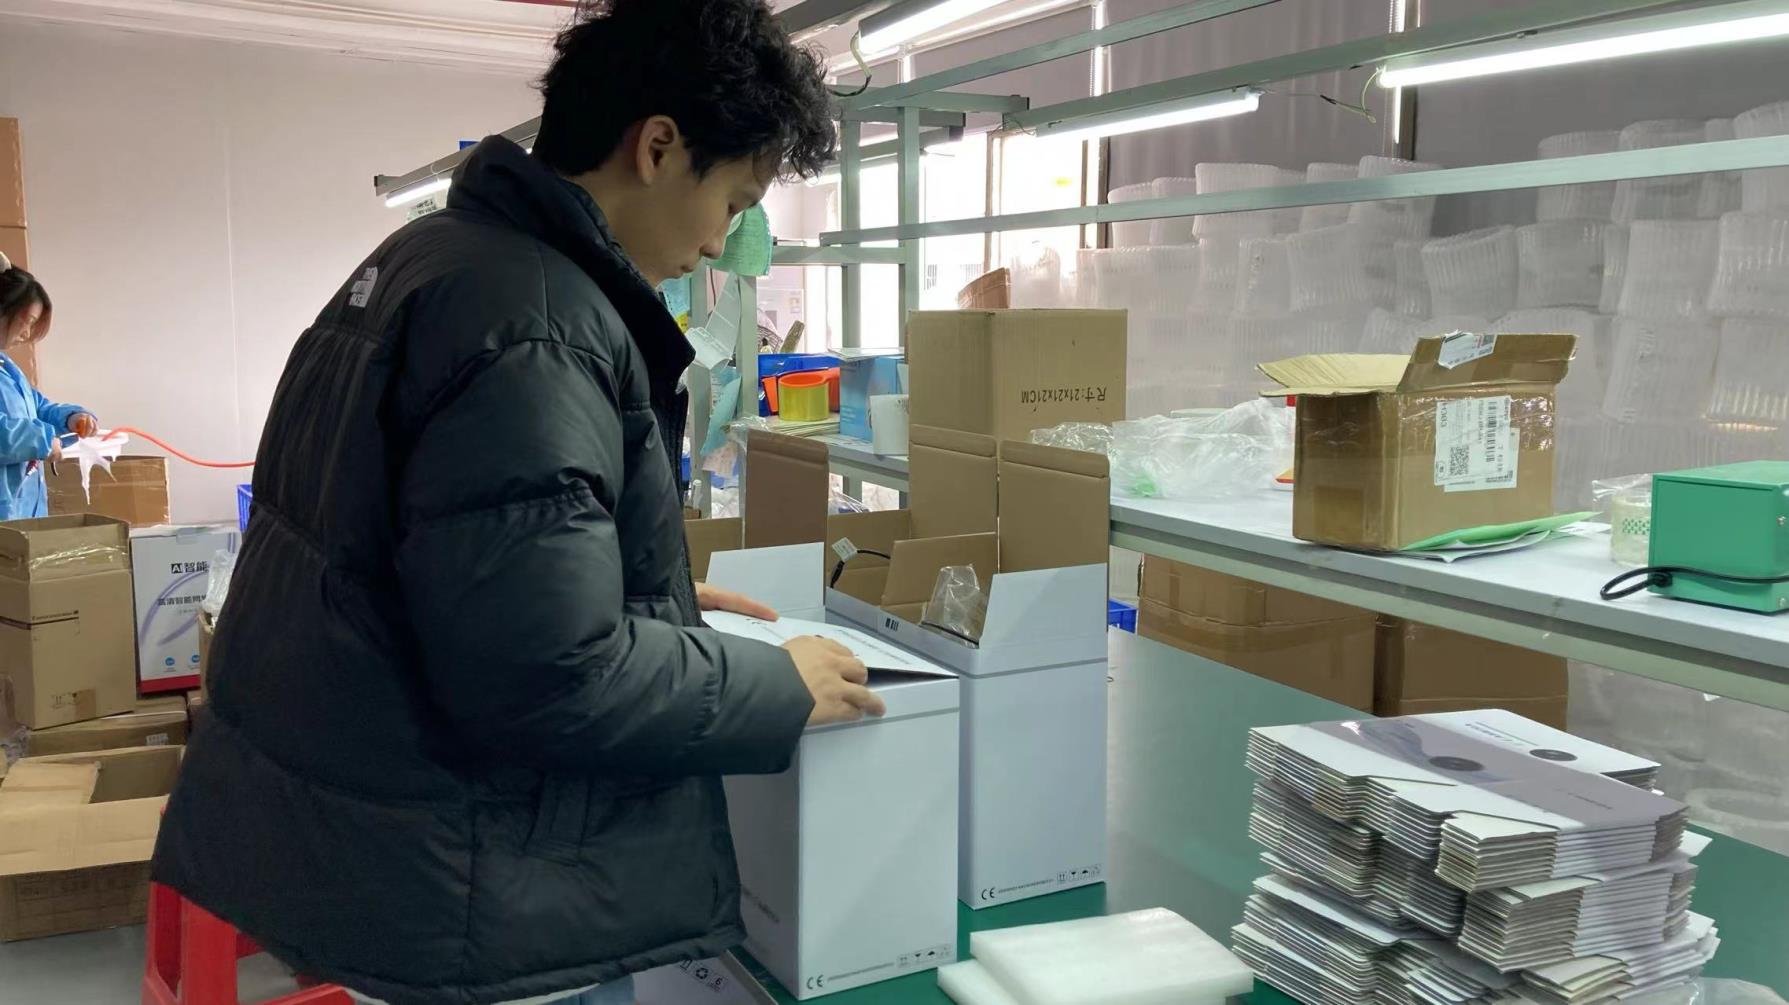
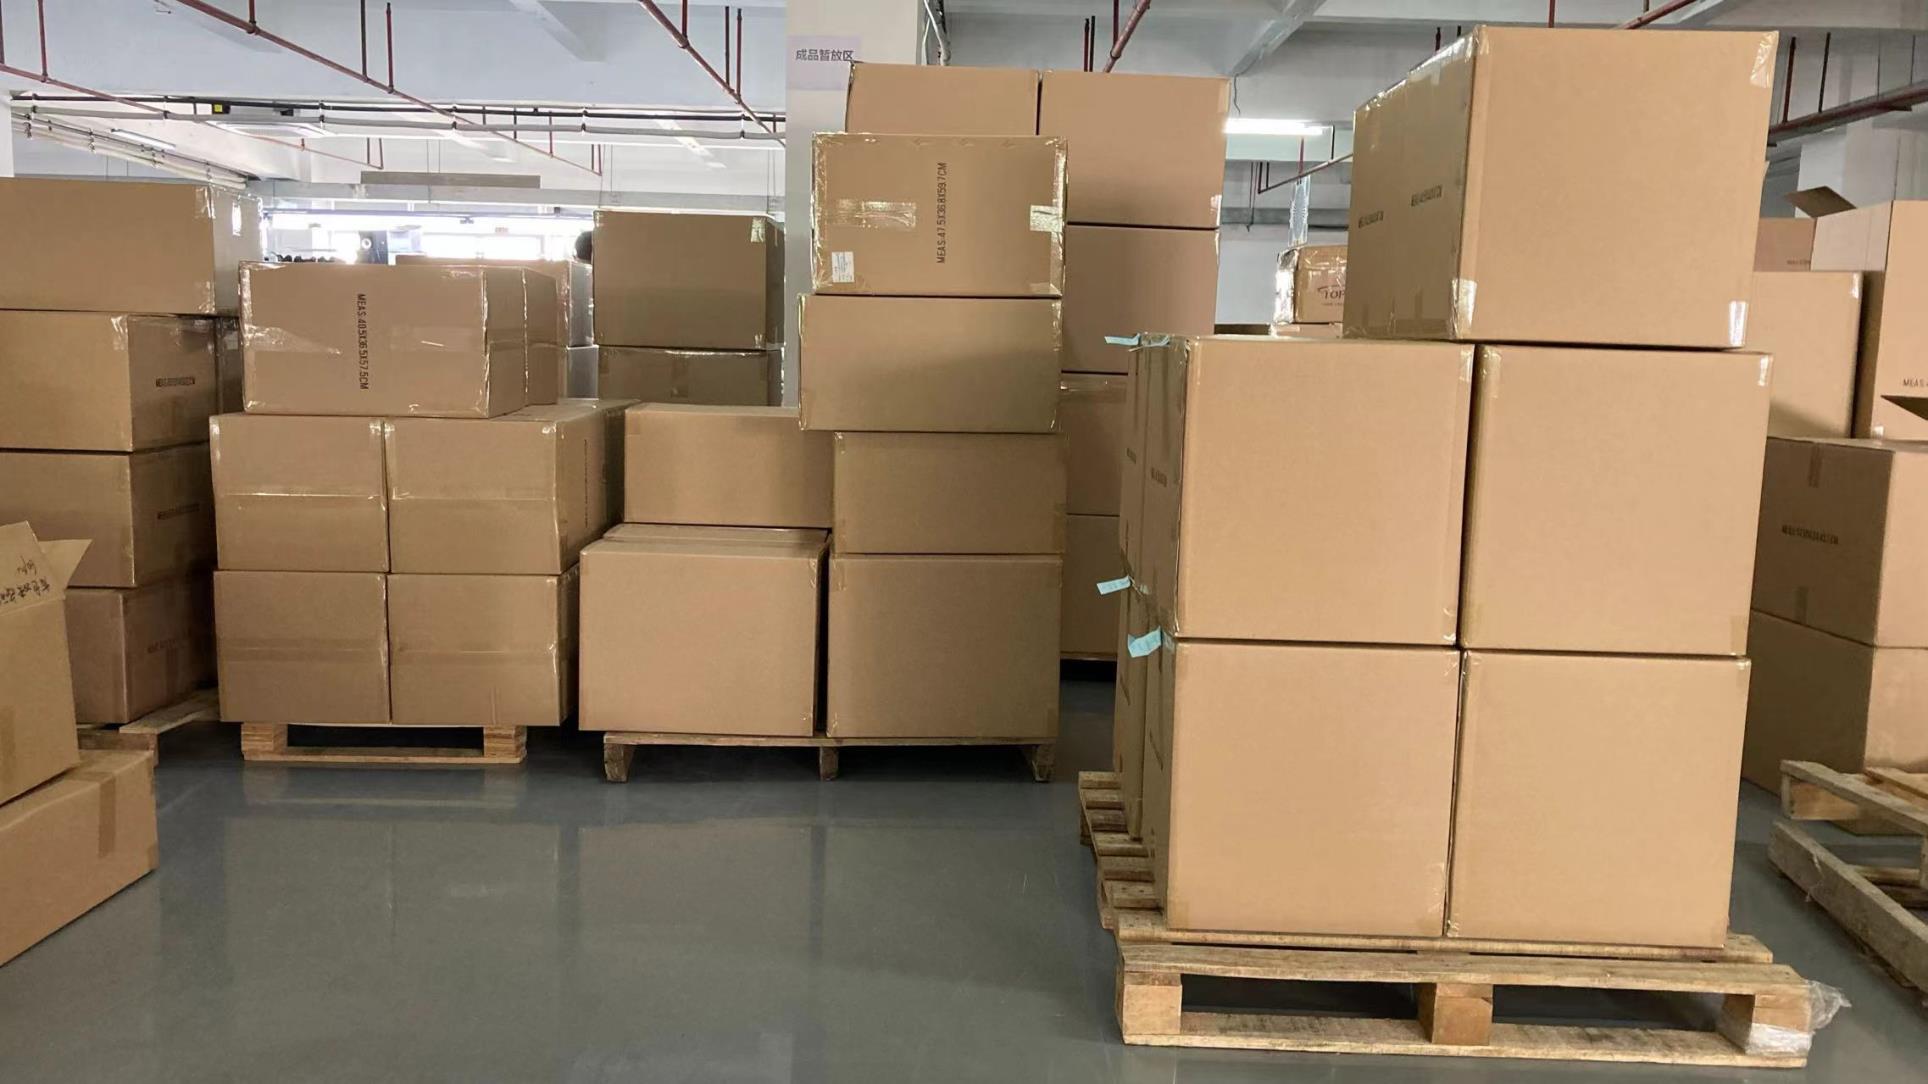
Witness our state-of-the-art manufacturing lines, precision assembly, thermal aging tests, and stringent quality inspections.
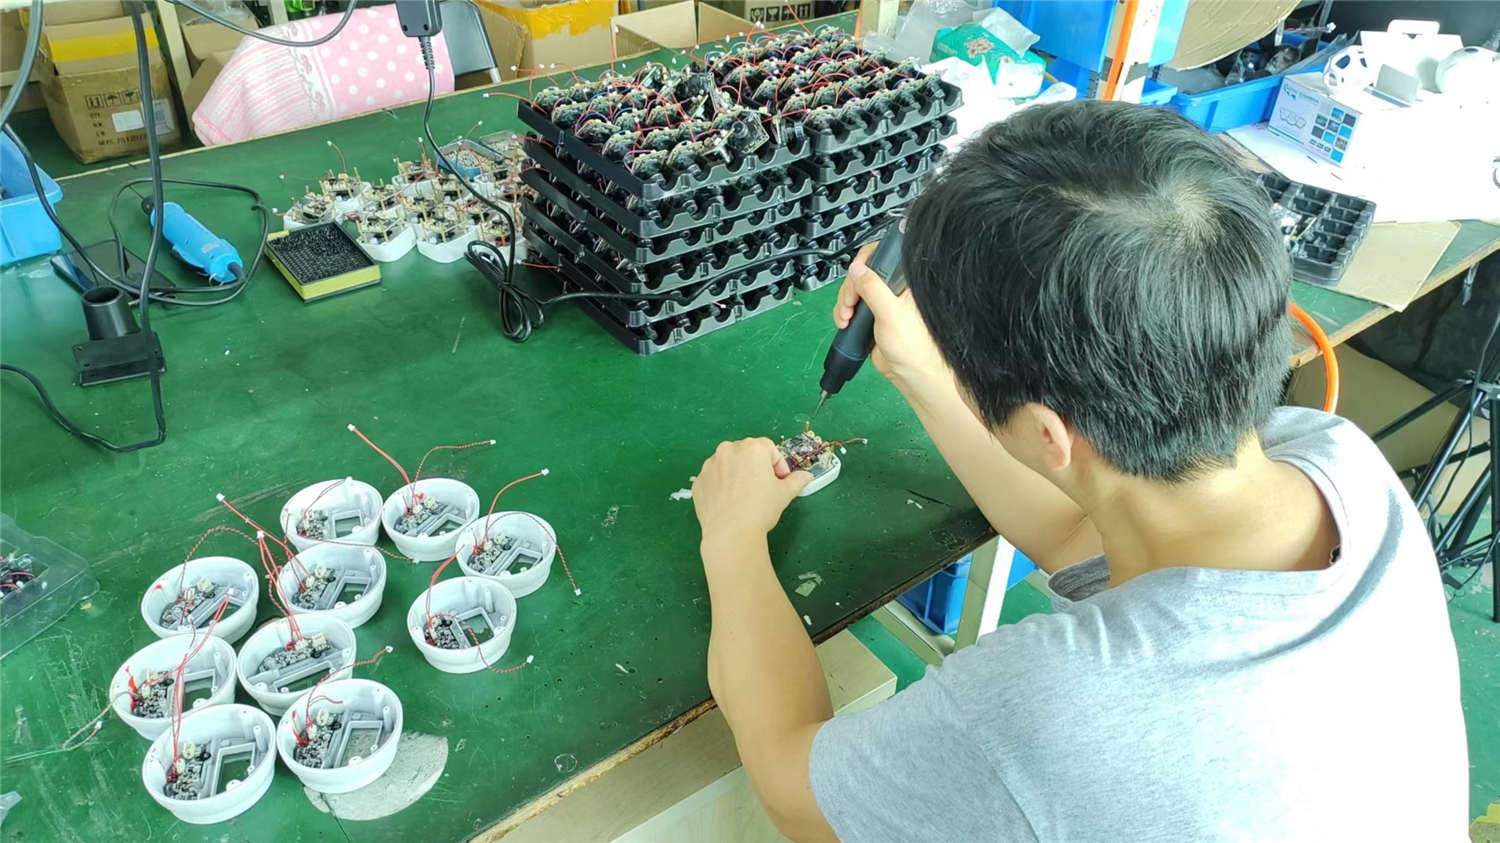
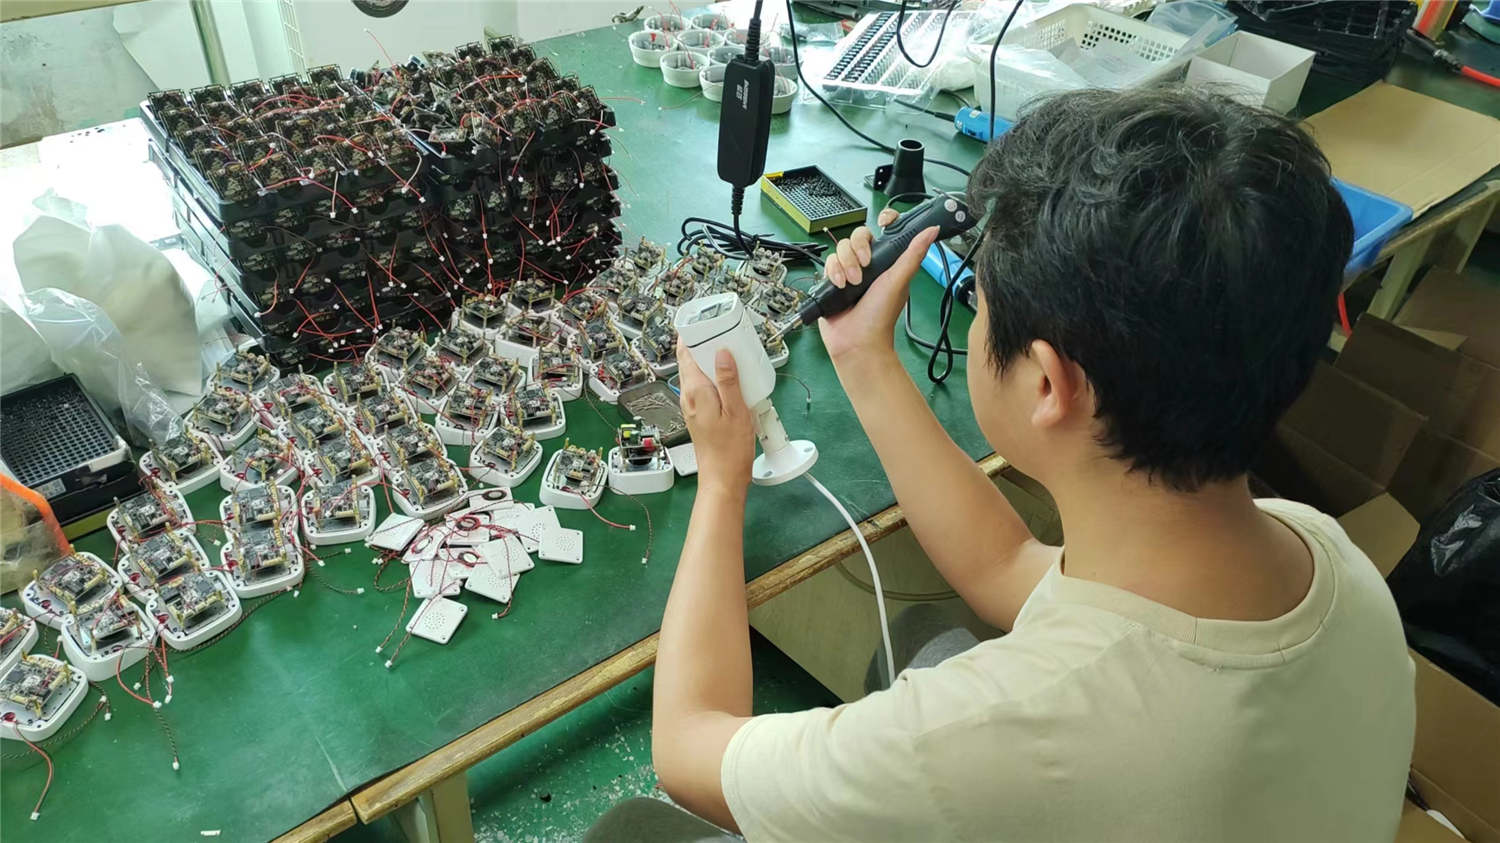
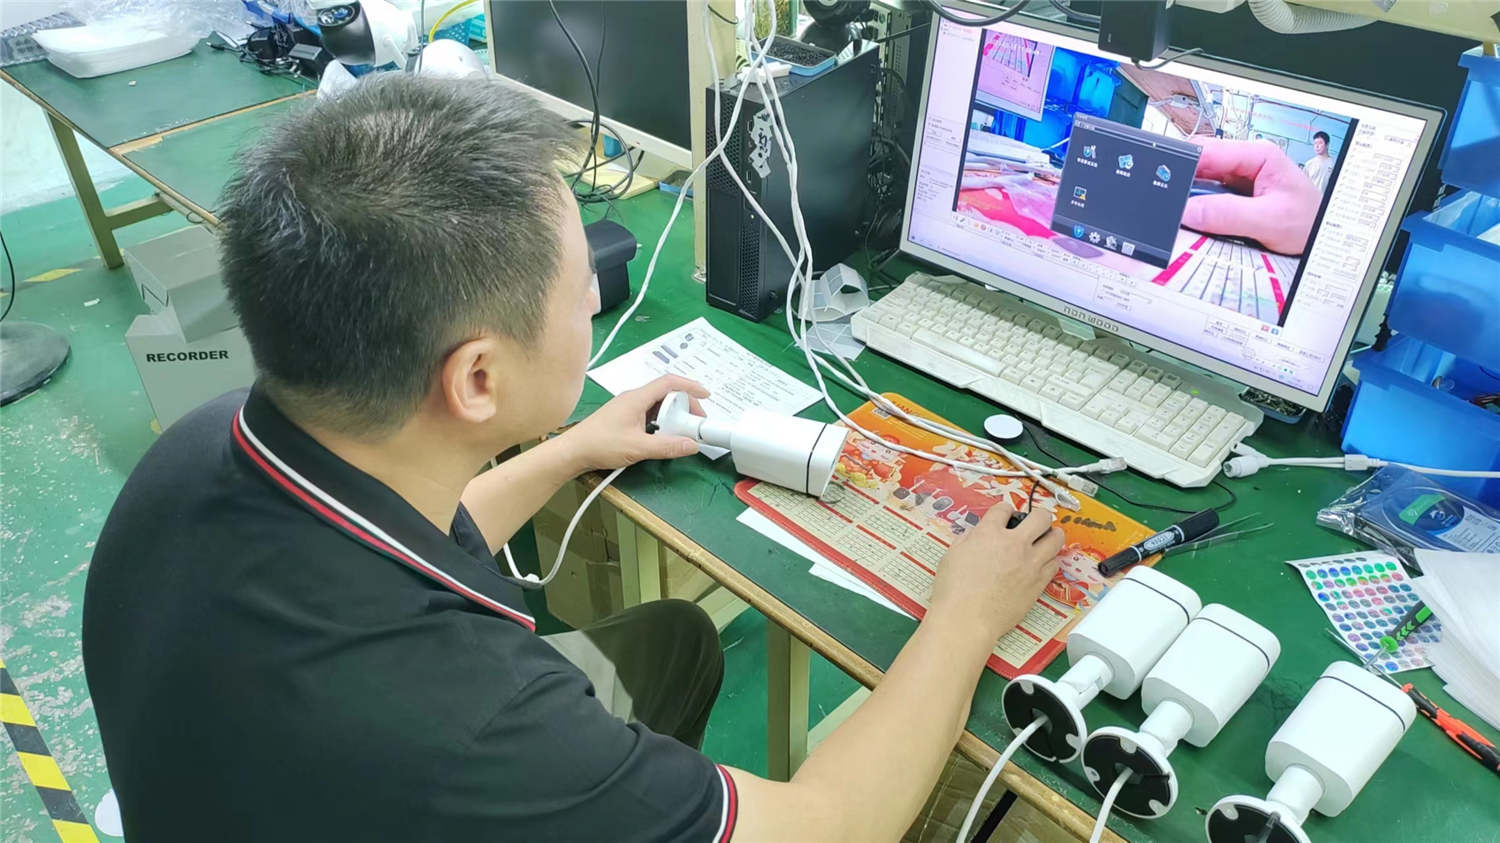
Expert answers regarding our integrated monitoring stations, custom manufacturing capabilities, and global partnership standards.
Our stations combine military-grade dual-spectrum thermal optics, carrier-grade wireless base stations, and robust solar/battery power options, backed by 15+ years of dedicated R&D and strict ISO9001/CE/FCC quality standards.
Yes! We offer complete OEM and ODM engineering services, tailoring optical lenses, thermal sensors, pan-tilt mechanical payloads, and firmware integrations to meet specific regional tender or industrial requirements.
All our products undergo rigorous testing at authorized inspection centers and carry international certifications including ISO9001, CE, RoHS, and FCC, ensuring seamless regulatory compliance worldwide.
Every unit undergoes extensive high-low temperature aging tests, waterproof/dustproof verification, salt-spray anti-corrosion checks, and functional stress testing before leaving our advanced manufacturing facility.
 HawkEye Camera